Each component that comes from the CNC mill or lathe carries a cost tag that is decided before machining starts. The design made in CAD defines how many tools are needed, how many times the component should be resetting, and how carefully the machinist has to move to prevent breaking a cutter or leaving a bad surface.
Minor adjustments in design can cut manufacturing charges high without affecting the part’s function. Here, 7 factors explain wall thickness, radii, hole depth, tolerances, threads, and setups, the points where a DFM review normally finds the most savings.
Wall Thickness, Internal Radii, And Why Geometry Fights The Cutter
Working with a custom CNC machining service at the start of the design phase often shows wall thickness errors before high charges.
Metallic walls are normally over 0.8 mm and plastic walls above 1.5 mm. Thin walls cause vibrations under cutting forces, a process known as chatter, which makes a rough surface and can push dimensions out of tolerance.’
The thin part forces slow light to pass; sometimes it takes three cycles for those parameters. Making a height-to-thickness ratio under 10:1 for aluminum and 4:1 for softer plastics, preventing the need for internal ribs or redesigns, and a wall 20 percent thick, compared to working at least minimum, often cuts scrap rates high. Sharp internal corners are a major cause of coming back high compared to the required value. The round end mill was not cutting square in the corner, so the shop needed small, slow tooling or a radius-matching design of tools.
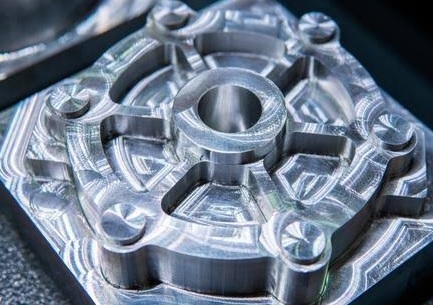
Internal radii of 1 mm or larger have common tooling, and values less than 0.5 mm force micro-end mills that wear faster and cost more per hour.
Hole Depth, Diameter Ratios, and Drill Wander
Deep holes are monitored by their depth-to-diameter ratio. Standard drills manage ratios up to about 4:1 comfortably.
Other than that, up to 10:1 or 12:1, shops need gun drills or peck-drilling cycles that retract repeatedly to clear chips.
Choosing drilling in real time as a hole at a 10:1 ratio can get 4 or 5 times longer than one at 3:1 because of repeated withdrawals. Shortening a hole or slightly increasing its diameter often moves it into a faster drilling category.
Tolerances & Thread Choices That Change The Machining Path
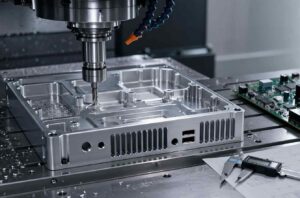
Tightening CNC machining tolerances other than that which the component needs is a high-speed method for inflating a quote.
Standard tolerances around ±0.1 mm work with normal roughing and finishing passes, and ±0.02 mm or tighter requires slower feeds, and in-process measurement.
Tight tolerances also increase rejection chances from thermal expansion and tool wear, so reserving them for the mating factor and leaving cosmetic dimensions at standard tolerance keeps most geometry on fast toolpaths.
Tapping is high speed for standard hole dimensions, but tap damage in blind holes is normally harder in alloys.
Thread milling charges high time per hole that generates high constant outcomes and causes tool cutting many thread sizes, minimizing tool variance on complex CNC machining projects.
A thread depth of about 1.5 times the diameter in metal offers full strength without unnecessary extra cutting.
Setup Count And The Hidden Cost Of Repositioning
Each flip or re-clamp added setup time unrelated to cutting. part machine bale in a single design at a low cost compared to single-needling, many since each setup needed re-establishing the part’s position based on the machine’s reference point.
Consolidating features over fewer faces, or using a five-axis machine to reach different sides without repositioning, minimizes labor and misalignment error.
Turning Cost-Conscious Geometry Into Better Parts
None of these seven factors needed sacrificing a part’s function. Wall thickness, radii, hole ratios, tolerances, thread depth, and setup count are all parameters the designer controls directly, and each has a number range where machining is fast and predictable.
Parts that manage these ranges move through a shop with standard devices, standard speeds, and fewer inspection delays, which make quotes reasonable without touching the part’s real factor.
Before The Quote: A fast Geometry Check
Before delivering the design for the quote, that helps to check these 7 points with a real drawing in hand compared to the memory of the guidelines. Check that there is no wall less than the metallic or plastic minimum, that the inner corner manages the radius the shop standard device can get, and that deep holes exist with a certain depth-to-diameter ratio for standard drilling.
Ensure that tight tolerances are used where features work with another component, that thread depth is not cut deeper than the strength requirement calls for, and that the component can be held and finished in as few setups as possible.
This type of self-review is important as a lightweight type of the DFM check a shop will run anyway, and catching these errors beforehand shows the quote that comes back indicates the part’s real complication compared to avoidable geometry options, often coming faster and closer to the final production cost
.